High Standards
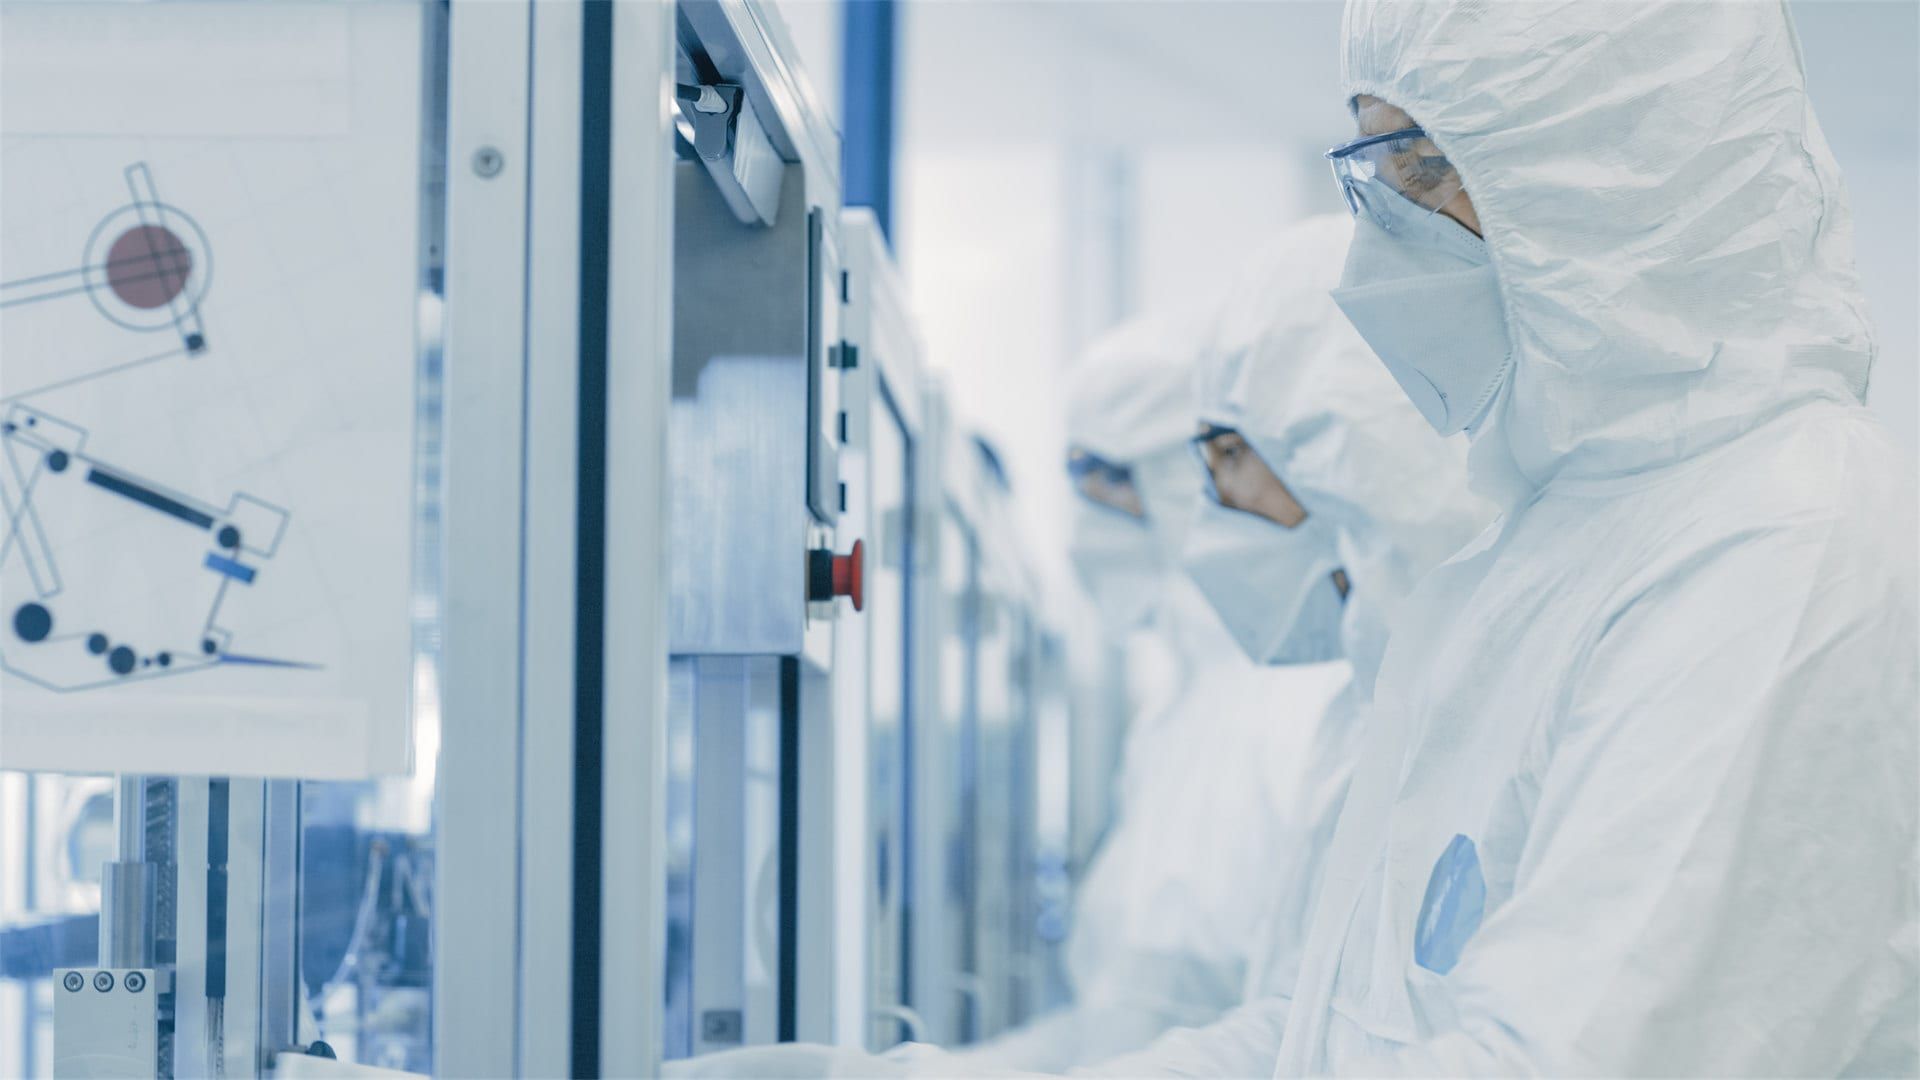
Products are tested and inspected before they are released to the market.
ABOUT MAXCLEAN
LEADING CLEANROOM CONSUMABLES SUPPLIER
MAXCLEAN has manufactured and developed cleanroom consumables for more than 35 years. Our complete production system covers research and development, material purchasing, manufacturing, inspection, packaging, and export.
Products are tested and inspected before they are released to the market.
Quality controls are applied across the multiple production stages behind every product.
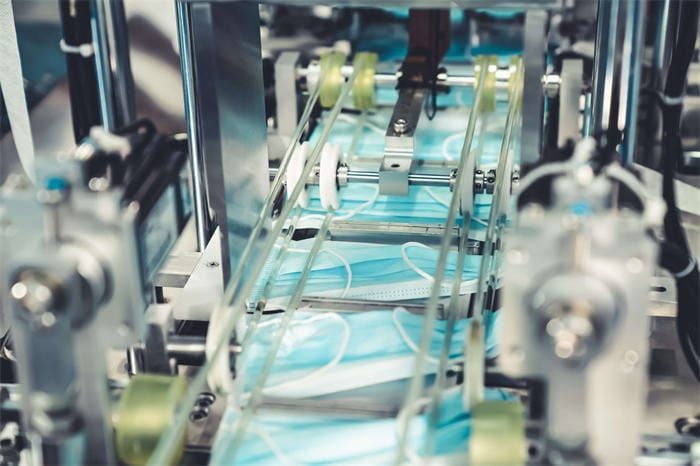
Our products support semiconductor, optics, electronics, medical, PCB, and other industries.
SUPPLY CHAIN DETAILS
MAXCLEAN supplies a wide range of cleanroom consumables and works as a one-stop supply chain solution provider. Integrated capacity helps us balance accessible pricing with dependable quality.
CUSTOM MANUFACTURING
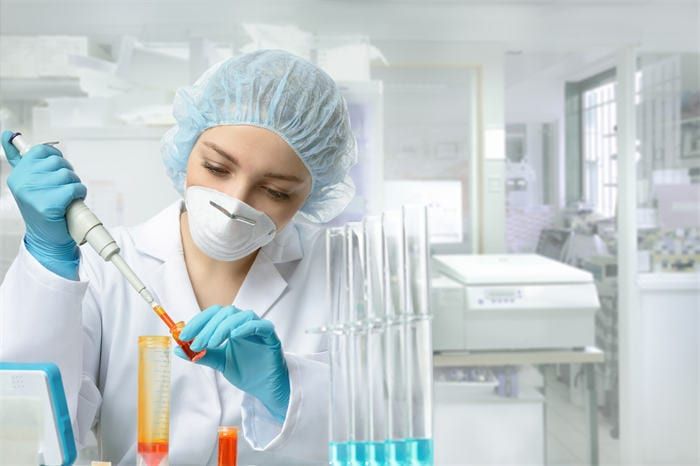
Customers have different aesthetic, branding, and packaging requirements. We provide branded, neutral, color, and monochrome packaging options to support distributor and private-label programs.
With an appropriate minimum order quantity, MAXCLEAN can help develop custom bags, cartons, and other packaging that protects each customer’s market position.
RESEARCH AND DEVELOPMENT
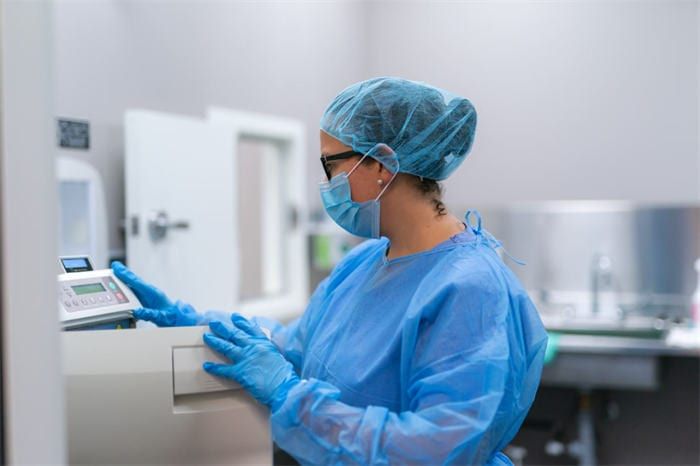
Our in-house research and development team studies the cleanroom market and works with users to identify the products, performance, and improvements they need most.
Close collaboration helps turn customer feedback into new products and practical upgrades that improve cleanroom efficiency.
CONTACT US
Get a quote, request a cleanroom consumables sample, discuss a cleanroom solution, or ask a question. MAXCLEAN is ready to help.
GET A FREE QUOTE